Food machinery, chemical and plant equipment, medical products and pump parts: stainless steel is machined more and more often in the Çukurova region. Yet a shop used to carbon steel often meets unexpected tool wear, sticking and poor surface finish in stainless. This article explains what makes stainless difficult and how to deal with it in practice.
Types of stainless steel
Tool makers group stainless steels as ISO M, but the types within the group behave very differently:
| Type | Example | Machinability |
|---|---|---|
| Austenitic | 304 (1.4301), 316L (1.4404) | Strong tendency to work harden and stick; the most common type |
| Ferritic | 430 (1.4016) | Relatively easy; behaves close to steel |
| Martensitic | 420 (1.4021) | Hardness depends on heat treatment; difficult when hardened |
| Duplex | 2205 (1.4462) | High strength; high cutting forces and heat |
Work hardening: cut, don’t rub
Austenitic stainless steels harden as they deform. If the tool rubs instead of cutting, the surface hardens and the next pass meets a harder layer. To avoid this:
- Don’t run the feed too low; a very thin chip leads to rubbing.
- Choose a depth of cut that gets below the layer hardened by the previous pass.
- Don’t let the tool dwell; avoid pauses when drilling and grooving.
- Don’t keep cutting with a worn tool: a dull edge smears instead of cutting and increases hardening.
Managing heat
Stainless steel conducts heat far less than carbon steel. Heat generated in cutting stays at the edge instead of leaving with the chip, causing fast wear, plastic deformation and coating damage. So:
- Start with a lower cutting speed than for steel and raise it while watching wear.
- Use plenty of coolant aimed straight at the cutting zone; high-pressure or through-tool coolant is best.
- In milling, low radial engagement (dynamic) strategies give the edge time to cool.
Tool geometry and coating
The most effective weapon against sticking (built-up edge) and work hardening in stainless is a sharp cutting edge.
- Positive geometry: Lower cutting forces and less heat.
- PVD coating: Keeps a thin, sharp edge; a common choice for milling and drilling stainless. In turning, CVD-coated grades developed for stainless also work well.
- The right chipbreaker: Austenitic stainless produces long, tough chips; match the chipbreaker to depth of cut and feed.
- Tough grades: Prefer breakage-resistant grades for interrupted cuts and duplex types.
Tips by operation
Turning: Varying the depth of cut between passes (e.g. 2.0 – 1.8 – 2.2 mm) stops notch wear from concentrating at one point.
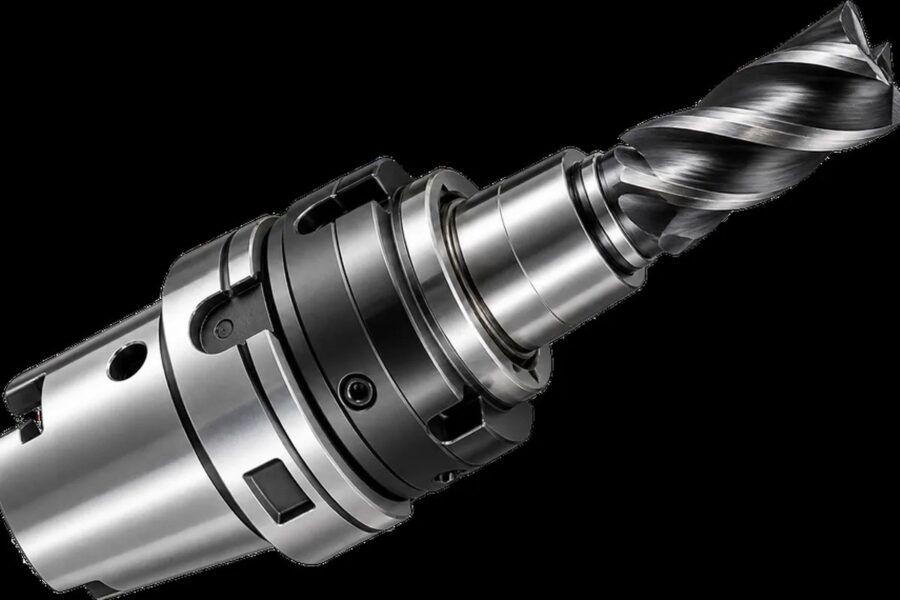
Milling: Multi-flute, variable helix end mills reduce vibration. Use climb milling.
Drilling: Through-coolant carbide drills and an uninterrupted feed are recommended. See our carbide drilling guide.
Tapping: Use a well-lubricating fluid and taps suited to stainless. Our tapping problems article lists the steps that reduce breakage.
Getting-started checklist
- Find out the stainless type and condition (annealed, hardened).
- Choose the recommended grade and cutting data for ISO M.
- Check coolant pressure and direction.
- Adjust the data on the first part by watching wear and chip shape.
- Define a tool change criterion; don’t keep cutting with a dull tool.